Precision Magnetic Components & Power Solutions
High-efficiency conversion platforms factory-audited to exceed European IEC and CE standards for demanding electrical topologies.
Engineering Perspective: Amplifier Transformer Sizing in Pyrenean Altitudes
Deploying professional sound reinforcement and high-end consumer amplification in the Principality of Andorra introduces unique operational constraints rarely encountered in low-lying maritime regions. Operating across high-altitude Pyrenean elevations—ranging from Andorra la Vella at 1,023 meters to ski resort summits above 2,500 meters in Grandvalira and Vallnord—demands non-standard thermal derating and specialized magnetic insulation strategies.
As altitude increases, atmospheric air density falls significantly. This reduction severely limits convective heat dissipation across magnetic cores and chassis assemblies. Conventional linear amplifier transformers manufactured for sea-level installations experience accelerated thermal degradation, localized coil hot-spots, and dielectric breakdown if standard thermal dissipation models are applied. Zelqo Power incorporates a standardized 12% to 18% thermal derating formula, utilizing low-loss grain-oriented silicon steel cores (CRGO) alongside Grade 200 Class H polyester-imide copper magnet wire. This ensures zero mechanical hum and thermal equilibrium under continuous heavy-duty acoustic amplification loads.
Toroidal Acoustic Isolation
Continuous annular grain-oriented ribbon cores eliminate air gaps, suppressing mechanical acoustic vibration (magnetostriction hum) below 28 dBA for ultra-pure signal clarity in audiophile preamps.
High Transient Response
Secondary windings optimized for symmetrical dual-rail power rails deliver instant current peaks for Class AB and Class D subwoofers without voltage sag during sudden dynamic audio transients.
Severe Environment Encapsulation
Epoxy potting options provide physical and dielectric isolation against mountain condensation, freezing ambient cycles, and salt/dust ingress typical of winter sports venues.
Localized Application Scenarios Across Andorra
Andorra's hybrid economy combines international luxury commerce, high-volume seasonal hospitality, and demanding infrastructure across complex mountain topography. Transformer reliability is non-negotiable for system integrators operating within the parish jurisdictions of Encamp, Canillo, Escaldes-Engordany, and Sant Julià de Lòria.
Alpine Resorts & Outdoor Stages
High-powered Public Address (PA) and acoustic line arrays require 100V/70V distribution transformers capable of withstanding ambient operating spans from -20°C to +40°C without core saturation or enclosure condensation issues.
Luxury Retail & Hospitality Systems
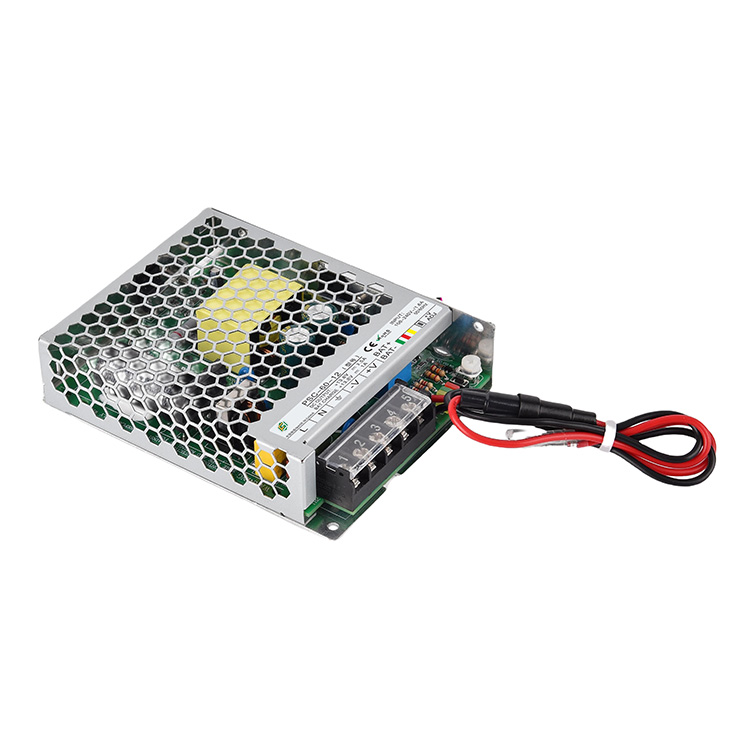
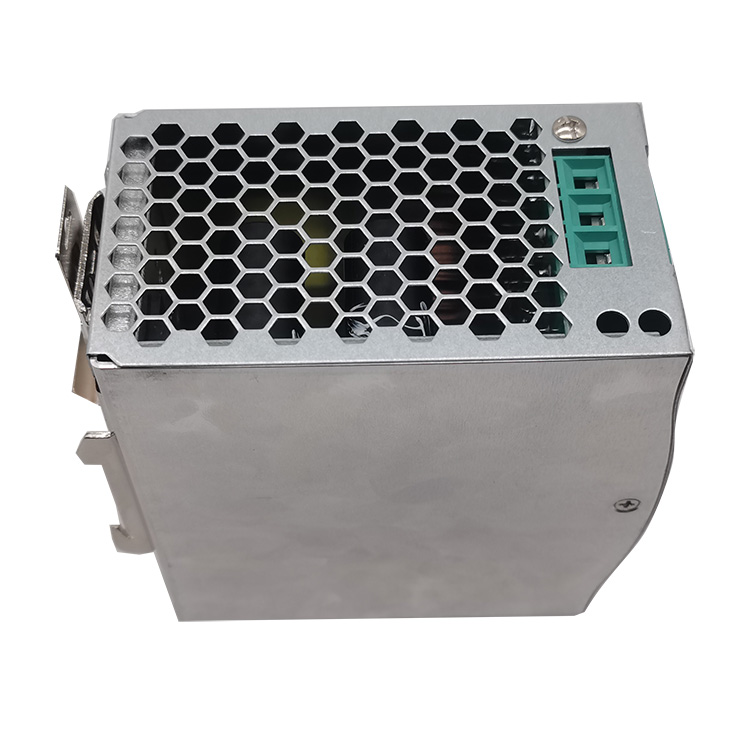
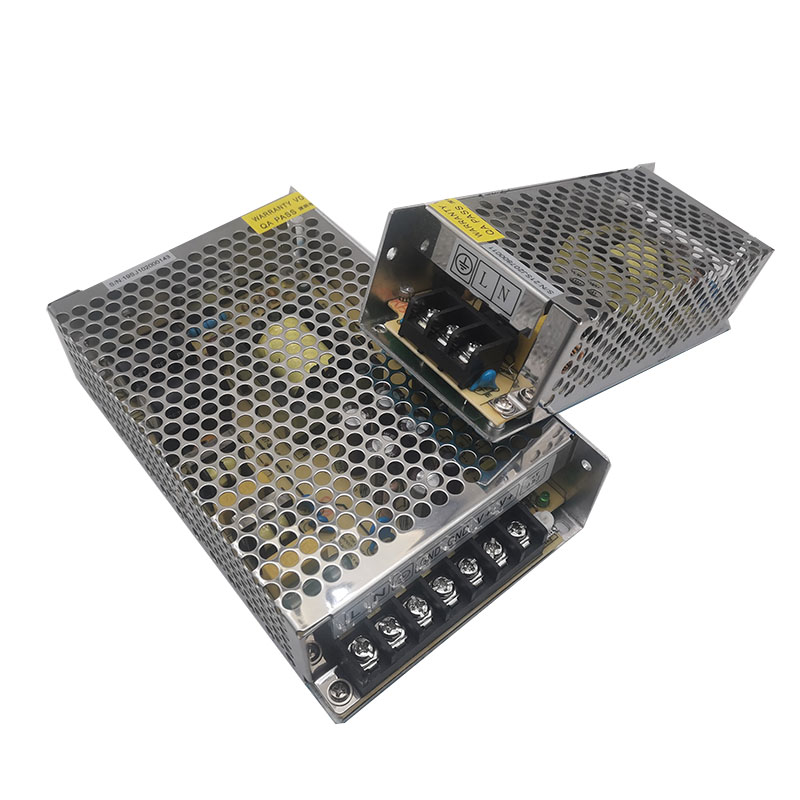
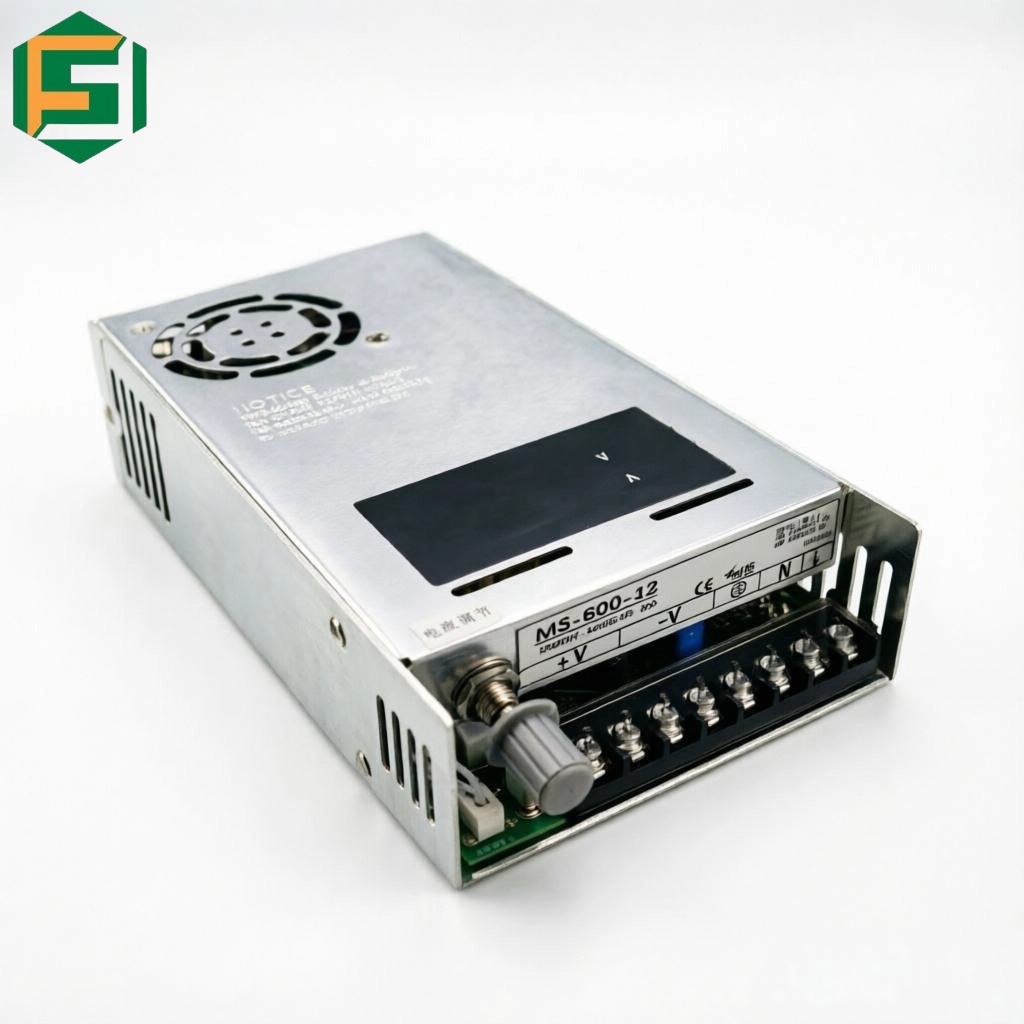
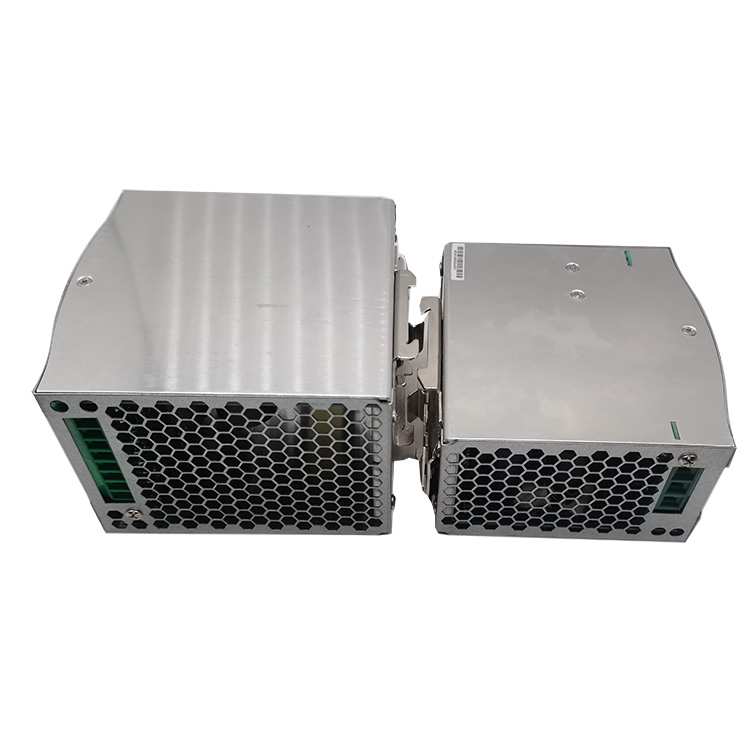
Commercial shopping avenues along Avinguda Meritxell require compact, ultra-quiet background audio amplification modules and DIN-rail power supplies that fit neatly into discreet false ceilings and tight electrical cabinets.
High-End Home Theaters & Studios
Custom residential chalets and private acoustic monitoring facilities in La Massana demand custom-wound toroidal transformers with copper foil electrostatic shielding between primary and secondary windings to stop line noise.
Macro Trends: Electrification & Audio Infrastructure in Andorra
Andorra is aggressively expanding its digital infrastructure, smart commercial zoning, and eco-friendly mountain resort networks. This macro shift creates distinct procurement trends for magnetic conversion devices:
1. Shift Toward Class D High-Frequency Switch Mode Magnetics: While classical linear toroidal transformers remain the undisputed standard for ultra-low noise studio reference monitors, commercial installations increasingly demand high-frequency planar and compact flyback transformers. These reduce the weight and thermal footprints of high-output multi-channel rack amplifiers installed in ski-station gondola operations and hotel complexes.
2. Compliance with European Low-Voltage and EMC Directives: Operating in close integration with French and Spanish border logistics means all electronic modules imported into Andorra must strictly align with CE, LVD (Low Voltage Directive 2014/35/EU), and EMC (Electromagnetic Compatibility Directive 2014/30/EU). Our transformers feature integrated Class F/H insulation and passed Intertek tests to guarantee immediate frictionless customs clearance and end-user safety.
Verified Manufacturing Strengths: Shaanxi Zelqo Power Co., Ltd.
Shaanxi Zelqo Power Co., Ltd., based in Xi'an, Shaanxi, China, operates an engineering-first production facility dedicated to toroidal transformers, low-frequency laminated transformers, high-frequency switch-mode transformers, and power adapters. Our on-site manufacturing, testing capabilities, and trade operations have been comprehensively verified by Intertek.
Intertek-Verified Plant
Full factory audit confirms verified manufacturing facilities, staff competencies, and direct raw material trace pathways.
Multi-Tier QC Testing
100% testing regimen: LCR digital bridge testing, DC low resistance checks, impulse winding tests, and hi-pot dielectric tests.
Custom OEM/ODM Engineering
Flexible primary/secondary voltage, electrostatic shielding, lead termination, potting resin, and enclosure customizations.
Direct Global Logistics
Experienced air and sea freight export management ensures door-to-door delivery into Andorra via Barcelona or Toulouse corridors.
Procurement FAQ for Andorran Engineers & Importers
Q: What core parameters are required for a custom amplifier transformer?
To prepare an optimized schematic, our engineering team requires input voltage and frequency (e.g., 230V AC 50Hz), secondary output voltages (loaded and unloaded), continuous and peak current requirements per rail, maximum enclosure dimensions, mounting preference (center bolt vs. fully potted PCB), and dielectric test targets.
Q: How do your transformers eliminate audible hum in audio gear?
We wind toroidal transformers on seamless, cold-rolled grain-oriented silicon steel cores. With uniform winding distribution, zero core air gaps, and optional inter-winding copper Faraday shielding, we prevent magnetostrictive vibration and keep electromagnetic stray fields well below industry thresholds.
Q: How does Zelqo handle logistics and customs clearances for Andorra?
Since Andorra is outside the EU customs union but operates under bilateral agreements, cargo is routed via transit corridors in Barcelona (Spain) or Toulouse (France). We furnish full commercial documentation, EUR.1 / certificates of origin, packing manifests, and HS code declarations to ensure rapid customs transit.
Q: Can you match existing chassis footprints for legacy amplifier repairs?
Yes. Our ODM/OEM services include reverse engineering and sample matching. If you are refurbishing or upgrading vintage amplifiers or legacy resort PA systems, we can wind custom low-frequency or toroidal units to match exact mounting dimensions, lead lengths, and terminal types.
Q: What is the typical lead time for engineering prototypes?
Standard design reviews take 24–48 hours. Upon confirmation of the electrical blueprint, custom prototype samples are wound, tested, and prepared for air-courier dispatch within 5 to 7 business days, accompanied by complete test verification sheets.